The systems that keep a plant running connected, safe and inspection-ready
When your network drops, your fire panel misreads a zone, or access control fails on a night shift, you do not lose convenience. You lose output, and sometimes your safety case. Yakkaservices designs, integrates, tests and supports the building systems behind your factory under one contract: the network, security, building management, and fire and life safety to NFPA 72 (2022). You get one team accountable for how they work together, and for the certificates your factory inspector asks to see.
What we sell, and when we are not your best option
Yakkaservices integrates the building and safety systems behind a plant. Here is where that work fits, and where it does not.
When we are the right fit
When a plant needs several systems designed, integrated, and certified together, and when one team is accountable for how they work as a whole.
When a single-system specialist fits better
If you need to replace one system on its own, a single fire panel or one camera run, a focused specialist contractor will often do it faster. That is the right call, and we will tell you when it is.
When you want an automation or MES vendor
If you are buying machine automation, a SCADA or MES platform, or production-line robotics, that is operational technology, and you want an industrial automation vendor. We design the network, security, building management and fire systems that sit around your production line, not the line itself.
Why manufacturing is different
What makes a plant's building systems different
A line that stops costs money by the minute
Your plant runs in shifts, often around the clock. When the network drops, a power feed trips, or an access gate jams, the line behind it stops, and the cost shows up as lost output every hour until it restarts. Your building systems carry that load quietly, which is why a fault is easy to miss until production feels it.
A factory carries rules an office does not
The Factories Act, your state factory rules, and the local fire authority all inspect a plant before it runs and while it operates. They check your fire detection, suppression, emergency lighting and exits, and they expect records. A plant also mixes uses an office never does: production halls, material and chemical stores, utilities, and sometimes hazardous zones, each with its own rule.
One event has to move people and protect plant at once
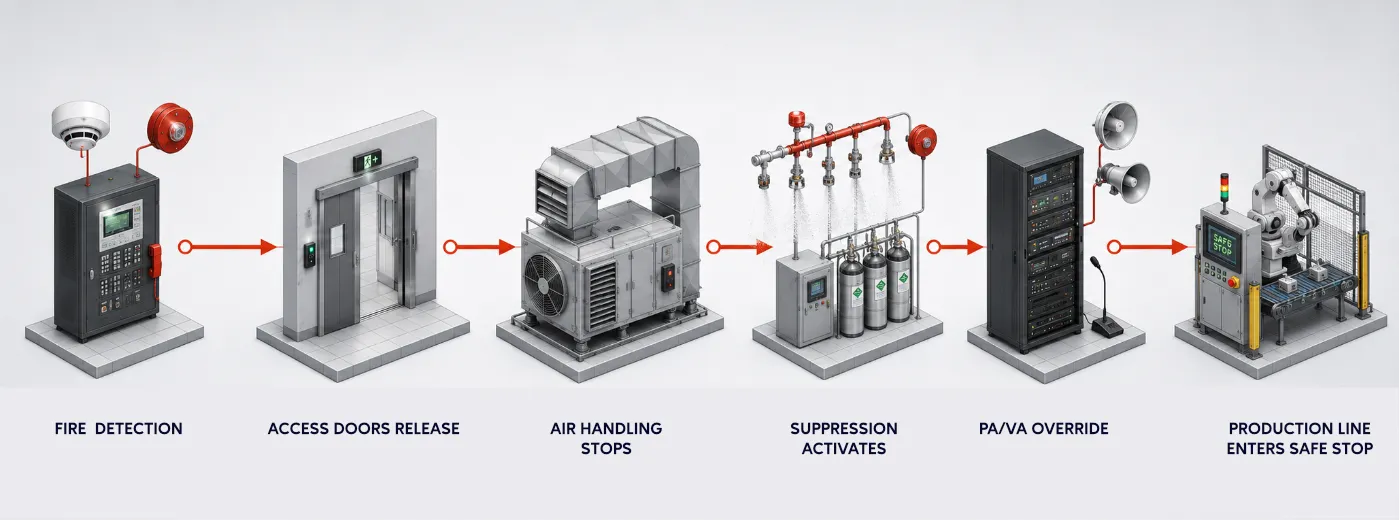
A fire in a storage bay has to alert the whole site, release the right doors, stop the air handling that would feed it, and start suppression, while staff in a separate hall keep a clear way out. That only works when your detection, suppression, public address and access control act as one system, not five that were installed separately.
Critical systems
The systems that keep a plant running
Every line, store and office in your plant rides on the same physical infrastructure. We design, integrate and certify these six systems so they work together as one connected plant, not just alongside each other.
Plant network & structured cabling
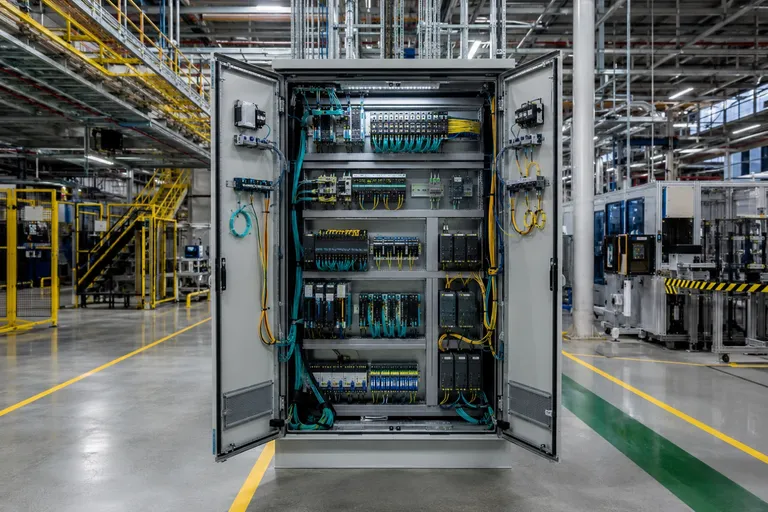
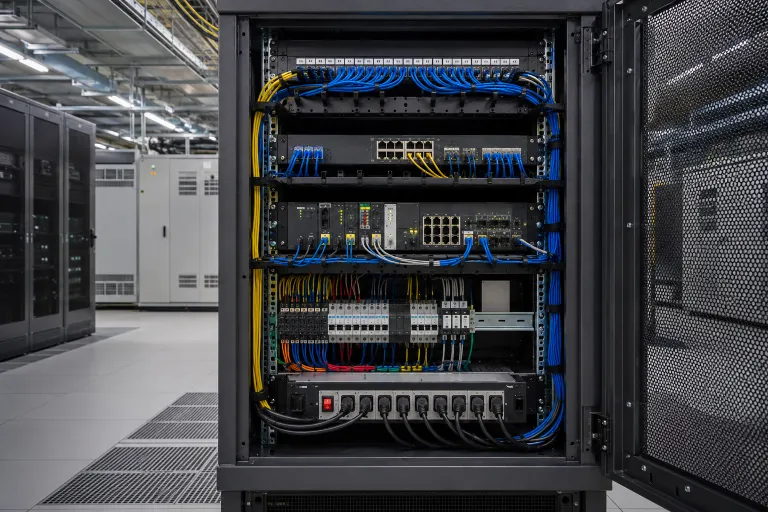
Every system in your plant rides the same network: production data, CCTV, access control, the phones and the office floor. We design and certify the cabling to TIA-568-D (2018) and ISO/IEC 11801:2017, run for the heat, dust and distance of an industrial site, with the resilience that keeps a line online when a switch or link fails.
A plant has gates, docks, stores and a chemical room that each need a different rule about who gets in. Access control and CCTV let you set those rules by zone, role and shift, log every entry, and watch the perimeter and loading bays. Lock-down and after-hours logic is designed in, not added after a theft.
Beyond the camera, your plant needs to know when a fence is breached, a gas leaks, or a store overheats. Intrusion detection, gas sensors and environmental monitoring feed the same platform, so an alarm reaches the right person on the right device, and a leak or a hot store is caught before it becomes a fire or a stoppage.
Energy is one of your largest controllable costs, and a plant wastes it where no one watches: idle compressors, oversized ventilation, lighting in empty bays. The BMS controls HVAC, compressed air and lighting, and shows energy use by line and by area. Built on BACnet and Modbus, and reported to ISO 50001 so the savings are measured, not assumed.
A factory fire moves fast through stored material and machinery, so detection has to be early and suppression has to match the risk. Your addressable fire alarm triggers the right doors, dampers and suppression in sequence, to NFPA 72 (2022) and EN 54, with sprinkler and special-hazard suppression to NFPA 13 where the risk needs it, and the commissioning evidence the fire authority asks for.
A shift cannot hear a wall siren over plant noise. We integrate public address and voice alarm so a fire event overrides routine paging with a clear, intelligible instruction by zone, loud enough for your floor, with EN 54-16 voice alarm and the meeting-room and training AV in the same scope.
Where plant systems go wrong, and how the failure is prevented
Four failures that appear at commissioning or after handover. Each one is preventable at design stage.
01Failure 01
Fire and suppression tested in isolation, not together
The fire alarm passes on its own, the suppression passes on its own, and nobody runs them together until the fire authority does. On a plant that means a failed NOC inspection on cause-and-effect, and a start date that slips while you re-test. We have been called to sites where the alarm sounded but the dampers never moved and the suppression never armed.
Consequence
A failed fire NOC inspection, and a production start that slips while you re-test.
Prevention
A written cause-and-effect matrix agreed early, then a full integrated test before the authority visits, not during it.
02Failure 02
Energy monitoring that shows a total, not a cause
A BMS that reports one site-level number tells you the bill went up, not which line, compressor or air handler did it. You pay for the waste for months because nothing points to the source.
Consequence
Months of avoidable energy cost with no way to find the source.
Prevention
Metering by line and by area in the BMS, reported to ISO 50001, so a rise points to a machine, not a mystery.
03Failure 03
Access and CCTV that record but do not alert
Cameras and card readers log everything and alert no one, so a breach at a gate or a tailgate into the chemical store is only found the next morning on playback. In a plant, that is a stolen load or a safety incident discovered too late to act on.
Consequence
A theft or safety incident found the next morning, not the moment it happened.
Prevention
Design the alarm and escalation rules first, so a breach reaches the right person live, then commission against real response targets.
04Failure 04
Installation that takes a running line offline
Cutting over a network or pulling new containment through a working hall without a phasing plan stops production at the wrong time. The result is lost output and a shift working around your contractor instead of running the line.
Consequence
Lost output, and a shift working around a contractor instead of running the line.
Prevention
A phased plan agreed with your operations and maintenance teams, cutovers scheduled into planned shutdowns, and a tested fallback for anything a line depends on.
Integration
How the systems connect in a plant, and why that is the hard part
In a plant, the systems are only as good as the points where they meet. None of that happens by accident. It happens because the interfaces were drawn at design stage and tested before handover.
One integrated response to a single event
Fire detected in a bay
Access doors release
Air handling stops
Suppression arms
PA/VA overrides paging
Line gets safe-stop signal
When one team designs and commissions all of it under a single contract, those interfaces are one team's responsibility. When each system is a separate contract, the gaps between them belong to no one, until the day they fail.
Compliance is easier to judge when you can see it by system. Here is what each system we deliver is designed, tested and approved against. Every tab carries authority approval and test certification at handover.
The network everything else runs on
Structured cabling and the data backbone that carries every system in the plant, designed for an industrial environment and for growth.
Authority approvalTest certification at handover
Designed, tested & certified to
TIA-568-D (2018)
Structured cabling design and performance
ISO/IEC 11801:2017
Generic cabling for customer premises
IEC 60364
Low-voltage electrical installations
Across all of them, you receive the evidence at handover: test certificates, the fire cause-and-effect matrix, energy metering verified to ISO 50001, and as-built drawings.
FAQs
Plant systems: questions buyers ask us
The questions plant owners, project teams, and consultants ask before they specify.
A plant needs the physical infrastructure its machines, people and safety case depend on. That means structured cabling and the plant network, access control and CCTV, intrusion and gas detection, building management for HVAC and energy, and addressable fire detection with suppression. Your production machinery, PLCs and MES sit on top of this layer. We deliver the layer, not the automation that runs the line.
Not quite. A smart factory usually describes the production side: machine automation, sensors on the line, and the software that schedules and analyses output. We design the connected building and safety systems that production depends on, the network, security, energy and fire systems. They make a factory safe and efficient to run, but they are a different layer from the MES and automation a smart-factory software vendor sells.
They act on shared logic that is designed and tested before handover. When detection finds fire or a gas sensor trips, the system releases the right doors, stops the air handling feeding the zone, arms suppression in the affected area, and overrides paging with a voice instruction. The production line can receive a safe-stop signal at the same time. The interfaces are written into a cause-and-effect matrix and proven in an integrated test, not assumed.
Yes. The systems are designed and documented to support the Factories Act, your state factory rules, and the local fire authority's NOC. Inspection looks for evidence that fire and life safety systems were tested and commissioned, so we hand over the cause-and-effect records, test certificates and as-built drawings the authority asks for. Final approval also depends on your building and process design, which sits outside the systems scope.
Yes, with a phasing plan agreed with your operations and maintenance teams before any work starts. Cutovers are scheduled into planned shutdowns or low-activity shifts, anything a line depends on keeps a tested fallback, and the method statement is built around your safety rules. The aim is that a line never loses a system it relies on at the moment it needs it.
As early as the design stage, while the consultant is still setting the systems scope. Early involvement lets the cross-system interfaces, cable routes and fire-rated containment be designed in, rather than corrected on site later. If the project is already under construction, an integrator can still take it over, but the earlier the interfaces are agreed, the fewer surprises at commissioning.
Book a manufacturing facility assessment
A clearer scope for your plant, whether or not you work with us
Tell us about your manufacturing project and a senior engineer reviews it with you, then sets out what your systems need and where the risks are.
An engineer who has delivered plant systems contacts you, not a salesperson
You get a response within one business day
No cost and no obligation for the assessment
If a single specialist contractor is the better fit, we will say so
Tell us about your manufacturing project
Response within one business day. No cost, no obligation.